Chinese
 Español
 Francés
 Deutsch
 Русский
 العربية
 Português
 日本語
 한국어
 Italiano

Solar Process Heat up to 90 °C with Flat Plate Collectors: A Factory Feasibility Checklist
Solar Process Heat up to 90 °C with Flat Plate Collectors: A Factory Feasibility Checklist
A screening framework for plant energy managers and EPC engineers — how to tell a viable low-temperature solar heat project from a dead one before any design work starts.
A solar process heat flat plate collector system is a realistic option when a factory needs low-temperature hot water or preheating — broadly below 90 °C. Temperature alone, though, decides almost nothing. Plenty of plants sit inside the right temperature band and still make poor projects.
What separates a viable case from a dead one is the combination of a repeatable heat demand, usable unshaded area, a practical tie-in point, and a conventional fuel bill large enough that displacing part of it matters.
So the opening question is not "can a flat plate collector reach 90 °C?"
It is: where in this plant can solar displace the most conventional fuel without making the process harder to run?
Most of that can be answered before any engineering design, using six pieces of operating data. This checklist walks through the screening logic an EPC or plant energy manager can run in an afternoon.
1. Does Your Process Temperature Actually Fit a Flat Plate Collector?
Industrial heat spans a huge temperature range. Flat plate collectors are relevant at the bottom of it: hot water preparation, washing, process water, boiler feed-water preheating, and some drying duties.
The common shortcut — "flat plate below 60 °C, something else above" — is too blunt for project screening. It rejects workable projects and waves through bad ones.
Below 60 °C: the strongest starting point
Loads under roughly 60 °C are the easiest to investigate: wash and cleaning water, low-temperature process water, tank heating, boiler or hot-water-system preheating, low-temperature drying.
The temperature difference between absorber and ambient air stays moderate, which keeps collector efficiency in a comfortable region.
That still does not make the project economic. A plant needing hot water one hour a week is a worse candidate than one running a slightly hotter but stable daily load. Temperature qualifies the process; the load profile qualifies the investment.
60–90 °C: feasible, but the operating point decides it
This band needs real calculation, not a rule of thumb.
A collector can be rated well above 90 °C and still perform poorly at your duty, because useful output depends on the gap between working temperature and ambient, not on the nameplate ceiling.
Before ruling anything in or out, the engineer needs: collector inlet temperature, required outlet temperature, ambient temperature, local irradiation, efficiency at the expected temperature difference, flow rate, system losses, and the daily and seasonal load shape.
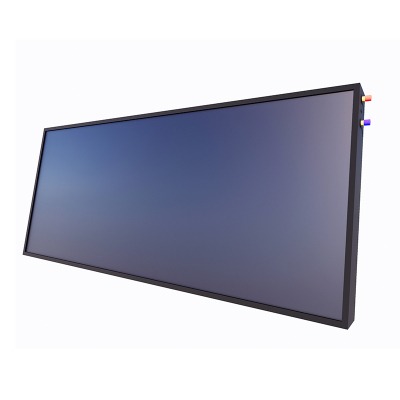
For reference on where the hardware ceiling sits: SOLETKS lists a maximum operating temperature of 100 °C for the FPC200-HM engineering collector, and 150 °C for the larger EFPC115 and EFPC150 modules. Those figures show flat plate should not be dismissed at 60–90 °C on principle.
A 150 °C ceiling says the product survives stagnation and high-temperature excursions. It says nothing about whether running near that point is thermally or economically sensible. Treat maximum operating temperature as a durability specification, not a design target.
Above 90 °C: compare technologies before you specify
Past the low-temperature range, technology choice becomes sensitive to climate, working temperature and system cost. Depending on the site, advanced flat plate, evacuated tube and concentrating options all deserve comparison — on delivered useful heat at the required temperature, not on maximum-temperature ratings.
| Required heat temperature | Initial direction | The question that decides it |
|---|---|---|
| Below 60 °C | Strong flat plate candidate | Is the load large and regular enough? |
| 60–90 °C | Flat plate worth evaluating | What is the efficiency at the real operating condition? |
| 90–100 °C | Detailed engineering assessment | Are the temperature lift and thermal losses acceptable? |
| Above 100 °C | Compare collector technologies | Which technology delivers the most usable heat at that temperature? |
The band tells you where to start the assessment. It does not tell you what to buy.
2. Pick the Heat Load, Not the Industry
A recurring planning error is asking whether an industry suits solar thermal. A textile mill, food plant or chemical site contains several thermal processes at completely different temperatures and schedules. The industry label predicts nothing.
Map the plant's heat consumers instead, and look for the lowest-temperature, most regular load that solar can serve without touching production control.
Boiler feed and make-up water preheating
A plant may need steam far beyond anything a flat plate field can deliver. That does not disqualify solar.
Rather than producing the final steam, the collector field raises the temperature of incoming feed or make-up water before it reaches the existing boiler. The boiler still does the final lift; solar replaces part of the fuel that lift used to consume.
The temperature of the final process does not have to equal the temperature supplied by the solar system.
For retrofits, finding a lower-temperature preheating stage is almost always more practical than trying to displace the primary heat source.
Wash and cleaning water
Plants heating water every working day are attractive because production is matched to a recurring thermal load rather than a seasonal one. Food processing, beverage production and similar operations with daily cleaning cycles fall here.
Before sizing anything, confirm the cold-water inlet temperature, required wash temperature, actual consumption, operating hours, and how all of it varies through the year. Annual water volume on its own is not a usable input.
Process and buffer tank heating
A tank that is heated repeatedly is often the cleanest tie-in available, because the tank itself buffers between variable solar output and process demand.
Feasibility turns on volume, start and target temperatures, required heat-up time, and whether the process control scheme tolerates a second heat source feeding the tank.
Drying: settle hot water vs hot air before anything else
Drying carries an extra decision, because not all dryers use heat in the same form.
If the process already circulates hot water through a heat exchanger, a liquid flat plate field integrates into the existing circuit. If the process needs heated air, solar air collectors for industrial and agricultural drying remove the water loop, the heat exchanger losses and the freeze-protection glycol entirely — a shorter energy path.
The boundary is narrower than most suppliers admit. In a SOLETKS agricultural drying deployment in Shanxi requiring a stable 50–70 °C air supply for a 445 m³ chamber, flat plate air collectors were ruled out and double-pass evacuated tube air collectors specified instead, because flat plate air designs are generally cost-effective up to around 45 °C and could not hold the target outlet temperature through a northern winter. The system pairs solar with air-source heat pumps under solar-priority control; reported season-level fuel savings and payback for that site are engineering estimates pending metered verification.
The first question on a drying project is therefore not which collector is more efficient. It is: does this process want hot water or hot air? That answer changes the entire system architecture, and getting it wrong late is expensive.
Not sure whether your process needs hot water or hot air?
Describe the drying or heating duty — chamber volume, target temperature, batch schedule and existing heat source — and we will advise which collector class fits before any sizing work begins.
3. The Six Numbers to Collect Before You Ask for a Design
A pre-feasibility assessment does not need a full engineering package. It does need plant data that has been measured rather than remembered.
1. Process inlet and target temperatures
Not "we need 80 °C water." Both ends: heating from 45 °C to 80 °C is a completely different load — and a different collector operating point — than heating from 10 °C to 80 °C.
2. Daily thermal demand
In kWh thermal per day or MJ per day if metered. If not, supply the raw inputs: daily hot-water volume, inlet and outlet temperatures, fuel or steam consumption attributable to the process, batch size and frequency.
3. Operating schedule and load profile
Two plants with identical annual consumption can need very different systems. Record shifts, weekday-only or continuous operation, seasonal patterns, batch irregularity. Hourly data is worth more than annual totals.
4. Current heat source and delivered cost
Identify exactly what solar would displace — natural gas, LPG, diesel, electricity, purchased steam — and use the plant's actual tariff, not a national average.
5. Available roof or ground area
"Roof area" and "usable collector area" are not the same number. Survey unobstructed area, shading, orientation, structural capacity, maintenance access, and any ground-mount option.
6. Distance from array to tie-in point
Locate the field relative to the boiler room, process tank, heat exchanger or storage. A good roof on the far side of a large site can be worse than a smaller area next to the heat consumer.
On point 3, the timing detail carries real design weight: daytime demand can often be served directly, while a load concentrated after sunset pushes the design toward storage and changes the cost base. On point 5, row spacing and pipe routing consume more area than most first estimates allow.
4. Reading a Collector Datasheet for a 60–90 °C Duty
Once a load passes screening, collector selection starts — and peak efficiency is the least useful number on the page.
Compare the parameters that shape the installed system. Using the SOLETKS range as a worked example of what to look for:
| Parameter | FPC200-HM | EFPC115 | EFPC150 |
|---|---|---|---|
| Gross area | 2.0 m² | 11.42 m² | 15.0 m² |
| Aperture area | 1.87 m² | 10.48 m² | 13.92 m² |
| Net weight | 30 kg | 235 kg | 315 kg |
| Working pressure | 0.6 MPa | 1.0 MPa | 1.0 MPa |
| Max operating temperature | 100 °C | 150 °C | 150 °C |
| Peak efficiency | 0.78 | 0.79 | 0.81 |
| Rated efficiency | 0.53 | 0.66 | 0.68 |
| Connections | G3/4 male, 4 | HTC40 quick connector, 2 | HTC40 quick connector, 2 |
Figures as listed on current product documentation. Confirm against the released datasheet version applicable to your order.
Four things in that table matter more than the efficiency figures.
Working pressure decides where you can tie in. A 0.6 MPa collector and a 1.0 MPa collector are not interchangeable when the loop connects to a pressurised industrial circuit. Check this against your system static head plus expansion before shortlisting anything — the specification detail sits on the engineering flat plate collectors built for pressurised industrial circuits page.
Module size trades installation cost against handling cost. Large modules cut the number of units, joints and potential leak points for a given field area. They also weigh 235–315 kg each, which pulls crane access, roof point loading and site logistics into the decision — worth checking the full module data for the EFPC large-format flat plate collectors before committing to a field layout. On a congested factory roof that trade can go either way.
Rated efficiency, not peak, is closer to your reality. Peak efficiency is measured with almost no temperature difference between absorber and ambient — a condition your 80 °C process will never see. The drop from 0.78 peak to 0.53 rated on the FPC200-HM is the honest illustration of that, and any supplier quoting only the peak figure for a process heat duty is answering a different question than the one you asked.
Heat loss coefficient predicts behaviour at temperature. The FPC200-HM is listed at 5.4 W/(m²·K) total heat loss coefficient. At higher operating temperatures this term dominates output, which is precisely why a datasheet without it is hard to evaluate for process heat.
The four numbers that actually shape an industrial field
Not the ones printed largest on the brochure.
The question to put to any manufacturer is not the maximum temperature. It is: what useful output does this collector deliver at our expected inlet temperature, ambient temperature and irradiation? If a supplier cannot answer with a performance curve, they are selling hardware, not a system.
Need performance data at your operating point?
Datasheet efficiency will not tell you what a collector delivers at 75 °C inlet in your climate. Send your duty conditions and we will provide the relevant performance curve, calculated output for your range, and the pressure and connection specifications for your circuit.
5. Where Should Solar Heat Enter the Existing Plant?
Solar process heat rarely means replacing the boiler. In retrofits the workable strategy is to add solar upstream or in parallel, leaving the existing plant as backup and final temperature control. The hydraulic detail, controls and commissioning sequence are covered in our guide on how to integrate solar thermal into an existing plant without replacing the boiler.
Preheat a storage or buffer tank
The solar loop charges a tank ahead of the existing heater, which then covers the remaining lift to setpoint. Attractive where suitable storage already exists.
Separate the solar loop with a heat exchanger
Necessary when the collector loop runs glycol, when freeze protection is required, or when process water quality must stay isolated. The exchanger adds its own temperature difference, so it belongs in the thermal design, not in the assumptions.
Solar in series ahead of the boiler or heat pump
Solar takes the first lift; the conventional system finishes. This is the configuration for plants that cannot tolerate any interruption of heat supply — production reliability stays with the existing equipment, and solar simply reduces its fuel input whenever useful heat is available.
Partial load reduction beats maximum solar fraction
For most factories, Option C is a more realistic objective than chasing a high solar fraction. Backup capacity and final temperature control stay where the plant already trusts them.
6. Is There Enough Usable Installation Area?
After temperature and load matching, area is the fastest way to kill an unrealistic concept.
Collector area ≈ target solar heat contribution ÷ expected useful yield per square metre
The trap is treating useful yield as a catalogue constant. It moves with site latitude and irradiation, operating temperature, collector performance, orientation and tilt, piping and storage losses, shading, control strategy, and — most of all — how well solar production overlaps the plant's demand hours.
Sizing a field from peak efficiency produces numbers that look precise and are not. The defensible sequence runs: heat demand → target solar contribution → local solar resource → performance at the actual operating temperature → collector area. Never the reverse.
7. What Actually Moves the Payback Number
"500 m² pays back in X years" means nothing without the project conditions behind it. Six variables do the work:
Solar resource. The same field produces materially different annual yield in different locations and seasons.
Fuel displaced. Replacing diesel or electricity is a different business case from replacing cheap gas. Use the plant's delivered cost, not a national average.
Operating temperature. Higher working temperatures widen the gap to ambient, raising losses and cutting useful efficiency.
Annual operating days — and their timing. A year-round plant can absorb more solar heat than a seasonal one, but when production runs matters as much as how often.
Utilisation. Heat only has value if it is used or stored. An oversized field dumping heat during low-demand periods earns nothing on the marginal square metre, which is why maximum solar fraction and optimal solar fraction are different targets.
Integration cost. Collectors are one line item. Mounting structure, piping, pumps, storage, heat exchangers, controls, insulation, installation and modifications to the existing plant frequently dominate the budget — and they are where feasibility studies most often understate cost.
8. When Flat Plate Solar Process Heat Is the Wrong Answer
A feasibility study earns its fee partly by killing bad projects. Compare alternatives when:
Nearly all useful heat must be delivered above the practical operating range of the proposed system.
Daytime thermal demand is small relative to the load, forcing heavy storage and depressing utilisation.
Production is highly irregular or seasonal, leaving the field idle for long stretches.
Usable installation area is insufficient — a large roof that is shaded, structurally marginal or occupied by HVAC plant is not area.
Recoverable waste heat already exists. Check this first. Waste heat recovery serving the same low-temperature load will almost always beat solar on cost.
The only available array location is far from the heat consumer.
Rejecting a poor application at screening is cheaper than forcing a technically possible system into the wrong process.
9. Pre-Feasibility Verdict: Go, Study Further, or Compare Alternatives
GO — worth a detailed feasibility study
Process heat mainly below 90 °C; demand occurring regularly during daytime production; high annual operating hours; sufficient unshaded roof or ground area; a meaningful current spend on gas, LPG, diesel, electricity or steam; and an identifiable preheating, tank or heat-exchanger tie-in.
FURTHER STUDY — engineering calculation required
The required temperature sits at the top of the 60–90 °C band; production varies sharply by season or shift; roof area is tight; the load profile is unknown; storage is likely needed; or the process carries strict temperature or water-quality constraints.
COMPARE ALTERNATIVES — do not specify a collector yet
Most useful heat is required substantially higher; annual utilisation would be low; there is no practical array location; another recoverable heat source is cheaper; or the process needs a different heat transfer medium.
Find the right load, not a reason to buy
The point is not to prove every factory should install solar thermal. It is to locate the load where solar cuts conventional fuel with the least disruption to production — or to establish early that no such load exists.
For scale reference on what a delivered flat plate field looks like: a SOLETKS engineering flat plate installation at the Changhong Intelligent Industrial Park in Mianyang, commissioned in 2020, supplies 138 tonnes per day of hot water to park offices and dormitories in a low-irradiance, frequently overcast climate, with reported annual reductions of roughly 300 tonnes of standard coal and 800 tonnes of CO₂. A separate 2023 industrial park system delivers 88 tonnes per day across offices, dormitories and production workshops.
Both of those are hot water loads rather than in-process heating, and both sit in China — so read them as evidence of array scale, climate tolerance and delivery capability, not as a proxy for your own process heat economics. The same applies to export track record: supplying collectors to buyers across 100+ countries demonstrates documentation, packing and logistics capability, not process heat performance at your duty point.
Ask any supplier to be equally explicit about which of their references are process heat and which are domestic hot water.
What to Send With Your RFQ
For a first-pass solar process heat assessment, six items:
Process inlet and target temperatures
Daily thermal or hot-water demand
Operating hours and load profile
Current fuel type and delivered energy cost
Plant location and available roof or ground area
Proposed tie-in or heat-use point
With those, an engineering team can put a range on collector type and area, propose an integration configuration, estimate the achievable solar contribution, and tell you whether a full technical and economic study is justified.
On industrial solar thermal, that conversation belongs before collector quantities and unit prices — not after.
Frequently Asked Questions
Can flat plate solar collectors produce 90 °C hot water?
In some applications, yes — but maximum operating temperature is the wrong basis for the decision. What matters is collector efficiency at your actual inlet temperature, ambient temperature, irradiation and required outlet temperature. Ask for the performance curve and the heat loss coefficient, then evaluate at your duty point rather than at test conditions.
Can solar thermal be used if the factory needs steam?
Often, yes — indirectly. Solar does not have to produce the final steam. It can preheat boiler feed water or make-up water before the existing boiler completes the temperature lift, displacing part of the fuel without altering the steam side of the plant. For retrofits this is usually the most practical entry point.
How much roof area does an industrial solar thermal system need?
There is no square-metre-per-tonne rule that survives contact with a real site. Required area depends on the target solar contribution, local irradiation, collector performance at operating temperature, and system losses. Calculate area from the plant's thermal load and demand profile, and confirm that the surveyed usable area — after shading, plant equipment, row spacing and access — is what you are actually working with.
Should a factory replace its existing boiler with solar thermal?
Generally not. Most retrofit designs keep the boiler or heat pump in place and use solar for preheating or partial load reduction. The existing plant retains backup capacity and final temperature control, which is what protects production continuity; solar reduces fuel consumption whenever useful heat is available.
Does the process need hot water or hot air?
Settle this before comparing collectors. If the process already circulates hot water through a heat exchanger, a liquid collector field integrates directly. If it needs heated air — most drying duties do — an air collector removes the water loop and its losses. Note the temperature boundary: flat plate air collectors are generally cost-effective to around 45 °C, and higher air temperatures typically call for a different collector class.
Request a Preliminary Solar Process Heat Assessment
Send your plant location, process inlet and target temperatures, daily heat demand, operating hours, current fuel type and delivered cost, and available installation area. Our engineering team returns an indicative collector type and area range, a proposed integration configuration, and an honest view on whether a full feasibility study is justified. If the load does not suit solar, we will say so.
Shandong Soletks Solar Technology Co., Ltd. · Company profile